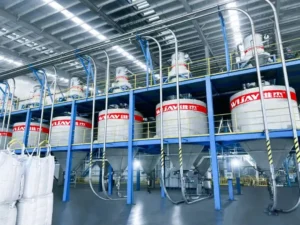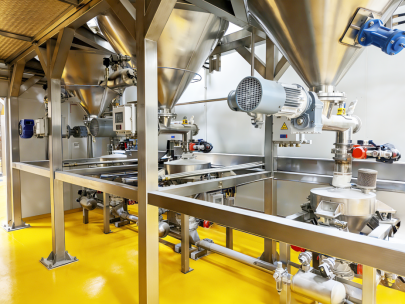
How to prevent bridging and rat-holing in feeder hoppers is one of the most common questions in bulk solids handling, and for good reason: fine powders, cohesive materials, and moisture-sensitive products routinely refuse to flow reliably through a feed hopper, and when they stop, feed accuracy goes with them. The material either bridges — forming a solid arch that completely blocks the outlet — or rat-holes, draining through a narrow vertical channel while the rest of the material along the walls sits frozen in place. Both failure modes degrade feeder performance, restrict discharge, and can shut a process down entirely.
This article explains why bridging and rat-holing actually happen, why the traditional fix comes with real trade-offs, and how a self-adjusting, non-contact activation approach solves the problem at the source instead of managing it after the fact.
Why Fine and Cohesive Powders Stop Flowing in the First Place
Bridging and rat-holing are both symptoms of the same underlying issue: the material’s own cohesive strength, combined with friction against the hopper wall, is enough to resist gravity at the outlet. Fine powders and sticky materials are particularly prone to this because their particles bond to each other more readily than free-flowing granular material does, and that bonding gets stronger under the weight of material stacked above it.
A bridge forms when that cohesive strength is enough to hold an arch of material in place across the entire outlet — the material above the arch simply sits there, supported by the arch rather than falling through it. A rat-hole forms when the material directly above the outlet keeps draining, but the cohesive strength along the hopper walls is enough to hold everything else in place, leaving a narrow vertical channel as the only active flow path. In practice, rat-holing is often the more deceptive of the two, because the feeder appears to be running and discharging material right up until the narrow channel empties out entirely and flow stops abruptly.
Why This Matters Beyond Just “The Feeder Stopped”
Both failure modes directly undermine feed accuracy, which is the actual metric most processes care about. A bridging hopper delivers no material until the arch is disturbed, at which point it can release an uncontrolled slug rather than a steady, metered flow. A rat-holing hopper delivers material inconsistently as the active channel narrows and widens, and once the channel empties, discharge stops with material still sitting untouched along the walls — material that may then sit long enough to consolidate further, making the next fill cycle even more prone to bridging.
The Traditional Fix and Its Real Costs
The long-standing solution to this problem has been a vertical agitator mounted inside the hopper — a mechanical shaft that physically stirs the material to keep it moving. It works, but it comes with genuine drawbacks that are easy to underweight until they show up in daily operation: it requires additional headroom above the hopper, which isn’t always available in an existing plant layout, and it’s difficult and time-consuming to clean, since the agitator sits directly inside the material path and has to be accessed from within the vessel for maintenance or product changeover. For food, pharmaceutical, or any application with hygiene requirements or frequent product changes, that cleaning burden is a recurring operational cost, not a one-time installation trade-off.
A Non-Contact Alternative: Activation From Outside the Hopper
A genuinely different approach addresses the same problem without putting anything inside the material path at all. The device mounts externally on the back wall of an extended hopper section, positioned above the feeder, and uses controlled frequency and amplitude to continuously activate the material inside the hopper — keeping it in gentle, ongoing motion without direct mechanical contact with the product itself.
Because nothing sits inside the vessel, there’s no internal component to clean during changeover, no headroom penalty from a shaft extending upward, and no direct wear surface exposed to abrasive or corrosive material. The activation happens through the hopper wall itself, which is a meaningfully different engineering approach from stirring the material directly.
Why Self-Tuning Matters as Much as Non-Contact Design
A fixed-frequency vibration device is only correctly calibrated for one specific fill level and one specific material flow behavior — which is a real limitation, since fill level changes constantly during normal operation and material behavior itself can shift with moisture content, particle size distribution, or batch-to-batch variation.
The more effective version of this technology includes a control unit that continuously monitors operating conditions and automatically adjusts frequency and amplitude to compensate for changes in hopper fill level and material flow behavior in real time. By actively maintaining optimal material movement rather than running at a fixed setting, the system prevents bridging and rat-holing before they form, rather than reacting once flow has already stopped — which is the core difference between activation as prevention and agitation as a response to a problem that’s already occurred.
A Case Worth Sharing: When Feed Accuracy Had Been Drifting for Months
We worked with a plant running a fine, moderately cohesive powder through a feed hopper equipped with a traditional vertical agitator. Feed accuracy had been gradually drifting out of tolerance over several months, and the operations team had attributed it to normal material variability, adjusting feeder calibration periodically to compensate rather than investigating a root cause.
The actual issue was intermittent rat-holing that wasn’t severe enough to stop the feeder outright, but was severe enough to create inconsistent discharge that the feeder’s calibration couldn’t fully correct for — the agitator was helping, but its fixed motion pattern wasn’t adapting to the specific combination of fill level and material behavior that was triggering the narrow-channel flow. Replacing the vertical agitator with an externally mounted, self-tuning activation system eliminated the rat-holing entirely across the hopper’s full fill range, and feed accuracy returned to its original tolerance without further recalibration. As a secondary benefit, changeover cleaning time dropped meaningfully, since there was no longer an internal agitator shaft to access and clean. The lesson: feed accuracy drift that gets treated as routine material variability is often actually an intermittent flow problem, and it’s worth investigating directly rather than compensating for indefinitely through recalibration.
Getting Reliable Feed Hopper Performance Without the Trade-Offs
Bridging and rat-holing are preventable, not just manageable, and the difference between the two approaches matters. A traditional vertical agitator addresses the symptom from inside the hopper, at the cost of headroom and cleaning complexity. A non-contact, self-tuning activation system addresses the same underlying flow problem from outside the vessel, adjusting continuously to actual conditions rather than running at a fixed setting — which is what makes it genuinely preventive rather than reactive.
FAQ
What’s the practical difference between bridging and rat-holing? Bridging is a complete blockage — a solid arch of material forms across the entire hopper outlet, and nothing discharges until it’s disturbed. Rat-holing is a partial failure — material drains through a narrow central channel while the rest of the material along the walls stays stationary, which can look like normal operation until the channel empties and flow stops abruptly.
Why do fine or cohesive powders bridge and rat-hole more often than granular materials? Fine particles bond to each other more readily than free-flowing granular material, and that cohesive strength increases under the weight of material stacked above it, which is exactly the condition that allows a stable arch (bridging) or a stagnant wall zone (rat-holing) to form.
Is a vertical agitator a reliable long-term fix for bridging and rat-holing? It can resolve the immediate flow problem, but it comes with real operational trade-offs — it requires headroom above the hopper and is difficult and time-consuming to clean, since it sits directly inside the material path. For hygiene-sensitive applications or frequent product changeovers, that cleaning burden is a recurring cost worth weighing against the alternative.
How does a self-tuning activation system know when to adjust? A control unit continuously monitors operating conditions inside the hopper and automatically adjusts frequency and amplitude in response to changes in fill level and material flow behavior, rather than running at a single fixed setting that’s only correctly calibrated for one specific condition.
Can feed accuracy problems be caused by intermittent flow issues that don’t fully stop the feeder? Yes, and this is a commonly overlooked cause. Partial or intermittent rat-holing can create inconsistent discharge that shows up as feed accuracy drift rather than an obvious stoppage, which is why accuracy problems attributed to “normal material variability” are sometimes actually a flow issue worth investigating directly.
WIJAY Systems specifies non-contact, self-tuning hopper activation as part of fully integrated feeding and metering systems — designed to prevent bridging and rat-holing before they disrupt discharge, without the headroom and cleaning trade-offs of a traditional internal agitator, across food, chemical, and other bulk material industries. If your feeder’s accuracy has been drifting and you’ve been compensating through recalibration rather than diagnosing the cause, that’s worth a conversation with our process engineering team.