
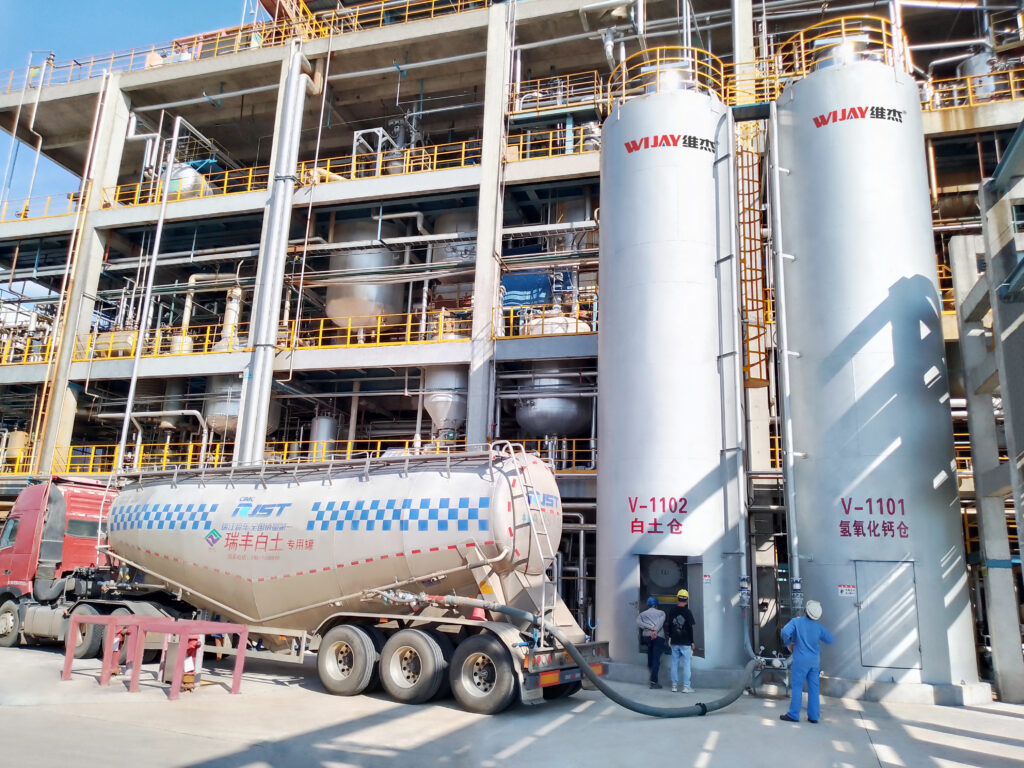
Across the full range of industry applications of pneumatic conveying systems — food processing, chemical manufacturing, plastics, minerals, pharmaceuticals — one question comes up more often than any other, and it’s rarely the one anyone expects: “What’s the solution, so I know how to budget the project?” It’s a fair question, but it usually gets asked before the harder, more important one has been answered — what’s actually causing the problem in the first place. Skip that step, and the budget conversation is built on a guess, not a diagnosis.
This article looks at the flow and conveying problems that show up across nearly every industry application of pneumatic conveying, why the same symptom can point to completely different root causes depending on the material and process, and why getting the diagnosis right before the capital request goes in is what actually determines whether the project needs to wait for next year’s budget cycle or can be resolved now.
The Symptoms Are Common Across Every Industry — The Causes Almost Never Are
Plants across very different industries tend to describe the same handful of problems in almost identical language: segregation and blending issues resulting in rejected product, material bridging or arching and rat-holing in a bin causing no-flow or erratic flow, transfer chutes plugging or wearing excessively, caking of powders generating customer complaints, and a plant needing higher throughput than the pneumatic conveying line, feeder, or transfer system can currently deliver.
What differs enormously, industry to industry and even plant to plant, is why any given symptom is actually happening. A food processing plant seeing intermittent bridging in a sugar silo and a mineral processing plant seeing the same symptom in a silica hopper are describing the same word — bridging — but the underlying cause, and therefore the correct fix, can be completely different. One might trace back to moisture-driven cohesion that changes seasonally; the other might trace back to a hopper angle that was never actually matched to the material’s wall friction characteristics. Treating “bridging” as a single problem with a single standard fix, regardless of industry or material, is exactly how plants end up spending capital on a solution that doesn’t address their specific root cause.
Where This Shows Up Differently Across Industry Applications
Food and beverage processing. Segregation and caking are particularly costly here because they show up as rejected batches and customer complaints, not just operational inefficiency — a segregated blend or a caked powder is a product quality failure, which means the cost of an undiagnosed root cause compounds through quality control, not just maintenance.
Chemical processing. Bridging, rat-holing, and transfer chute wear intersect with abrasiveness, corrosivity, and containment requirements that don’t exist in the same way elsewhere — a chute plugging issue in a chemical plant might be a material-handling problem, or it might be a symptom of a material that’s reacting or degrading in ways that change its flow behavior over time.
Plastics and polymer manufacturing. Throughput limitations on pneumatic conveying lines are common here, and the instinct is often to assume the conveying line itself needs to be bigger — when the actual constraint is sometimes upstream, at a feeder or transfer point that was never sized for the throughput the plant is now trying to push through it.
Minerals and abrasive material handling. Chute wear and plugging are routinely treated as an expected cost of handling abrasive material, when the actual cause is frequently velocity or geometry that could be corrected without accepting that wear as permanent.
Across all of these, the symptom vocabulary is nearly identical. The root cause almost never is — which is exactly why a standard fix applied without diagnosis so often misses.
Why Guessing at the Fix Is an Expensive Habit
Making a change without first determining the actual root cause is a genuinely costly form of trial and error, and it’s costly in ways that go beyond the failed fix itself. A capital project greenlit to solve the wrong problem still consumes budget, schedule, and internal approval effort — and when it doesn’t resolve the symptom, the plant is back where it started, except now with less budget and less patience for a second attempt.
The more useful distinction, and the one most plants skip straight past, is whether the actual fix requires capital spending at all. Some flow and conveying problems are resolved with a change that fits comfortably inside a maintenance or operations budget — a hopper liner change, a velocity adjustment, a chute angle correction — while others genuinely require capital investment in new or redesigned equipment. Without a proper diagnosis, there’s no way to know which category a given problem actually falls into, which means plants routinely either overspend on capital projects that a smaller fix would have solved, or underinvest in problems that genuinely need capital and keep absorbing the ongoing cost of a symptom that a maintenance-level fix was never going to resolve.
A Case Worth Sharing: When the Capital Project Wasn’t Needed at All
We worked with a plant that had already begun preparing a capital request to replace a transfer chute experiencing chronic plugging and excessive wear — the assumption going in was that the chute itself was undersized or poorly positioned for the plant’s current throughput, and the team was building a business case for a full chute redesign and replacement.
An on-site assessment before that budget request was finalized told a different story. The chute geometry itself was reasonably sound; the actual issue was that the material’s flow properties had shifted from what the chute was originally designed around — a supplier change upstream had altered particle size distribution enough to change the material’s cohesive behavior at the chute’s operating angle, without anyone connecting that supplier change to the plugging that started showing up around the same time. The fix wasn’t a new chute. It was a modest angle adjustment and a surface treatment change, completed within the plant’s existing maintenance budget, with no capital request required at all. The plant avoided a capital project that wouldn’t have solved the actual problem, and resolved the plugging faster than the capital approval process alone would have taken. The broader lesson: a symptom that looks like it obviously requires a capital fix sometimes doesn’t — but there’s no way to know without diagnosing the actual cause first.
What a Proper Diagnosis Actually Looks Like
Determining root cause before committing to a fix generally means an on-site engineering assessment that looks at the actual material’s flow properties under the plant’s real operating conditions, rather than assuming behavior from a similar-sounding material or a generic industry benchmark. It means examining the full system — hopper geometry, transfer points, conveying line sizing, feeder capacity — rather than assuming the symptom’s location is automatically the root cause’s location, since a throughput limitation that shows up at the conveying line is just as likely to originate at an undersized feeder upstream. And it means being honest about which category of fix the diagnosis actually points to: a maintenance-budget adjustment, or a genuine capital project.
That honesty matters more than it might seem, because it directly answers the budgeting question plants actually come in asking. Getting an engineered diagnosis before the capital budget cycle tells a plant whether the project genuinely needs to compete for next year’s capital funding, or whether the fix can be completed now, inside the budget that’s already available.
Getting the Sequence Right Across Any Industry Application
Whatever industry application of pneumatic conveying is involved — food, chemical, plastics, minerals, or anything else handling bulk solids — the sequence that actually works is the same: diagnose the root cause first, determine which budget category the real fix belongs to, and only then commit to a specific solution and its cost. Skipping straight to “what’s the solution, so I can budget it” inverts that sequence, and it’s exactly how plants end up spending capital on projects that were never going to solve the actual problem.
FAQ
Why do flow problems like bridging or plugging look the same across different industries but have different causes? Because the symptom describes what’s visibly happening — material not moving, a chute clogging — while the cause depends on the specific material’s properties, the equipment’s actual geometry, and how those two interact under the plant’s real operating conditions, all of which vary significantly by industry and even by supplier change within the same plant.
How do I know if a flow problem needs a capital project or can be fixed with existing maintenance budget? That distinction is exactly what a proper root-cause diagnosis is meant to answer. Some fixes — angle adjustments, surface treatments, velocity changes — fit inside existing maintenance or operations budgets, while others genuinely require capital investment in new or redesigned equipment. Without diagnosis, there’s no reliable way to know which category applies.
Can a supplier change to the same material cause a flow problem that wasn’t there before? Yes, and it’s a commonly overlooked cause. A shift in particle size distribution, moisture content, or other flow-relevant properties from a new material source can change how that material behaves in equipment that was originally sized for the previous source, even when the material is nominally “the same” on paper.
Is a throughput problem always caused by the conveying line being undersized? Not necessarily. A throughput limitation that shows up at the conveying line can originate upstream, at a feeder or transfer point that was never sized for the throughput the plant is now trying to push through the system — which means fixing the conveying line alone wouldn’t resolve it.
Why is an on-site assessment better than estimating a fix remotely? Because flow behavior depends on the material’s actual properties under the plant’s real operating conditions — moisture, temperature, equipment wear, and handling history all factor in — and those conditions are difficult to fully capture without direct, on-site evaluation of the specific system experiencing the problem.
WIJAY Systems engineers on-site diagnoses of bulk solids flow and conveying problems across food, chemical, plastics, mineral, and other industry applications of pneumatic conveying systems — determining root cause before recommending a fix, so you know whether a project belongs in next year’s capital budget or can be resolved now. If your plant is dealing with segregation, bridging, chute wear, caking, or a throughput ceiling and isn’t sure yet what the real fix requires, our process engineering team is glad to talk it through.








