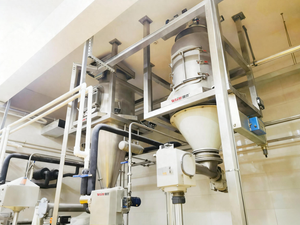
When a plant moves roasted peanuts, pelletized carbon black, or breakfast cereal, the enemy is impact. When it moves sand, glass batch, or refractory batch, the enemy is wear. At first glance, these look like opposite problems. In practice, they often point to the same solution: custom dense phase pneumatic conveying systems for fragile and abrasive materials. The key is not simply choosing “pneumatic conveying.” It is choosing the right conveying concept, velocity, pressure profile, pipeline route, and component details for the material in front of you.
I have seen plants try to solve both problems with dilute phase systems because they are familiar and low in initial cost. Then fragile products break, abrasive products eat through elbows, and maintenance becomes a monthly routine. I have also seen the opposite: a properly engineered dense phase system move both types of material with low degradation and long pipe life. The difference is design discipline.
Dense Phase vs. Dilute Phase: A Practical Comparison
Dilute phase conveying uses high velocity and a low material-to-air ratio. Particles are suspended and travel fast. This works well for non-abrasive, robust materials over short distances and low to medium rates. But high velocity is brutal on fragile pellets and abrasive particles. Breakage rises, and pipe wear rises even faster.
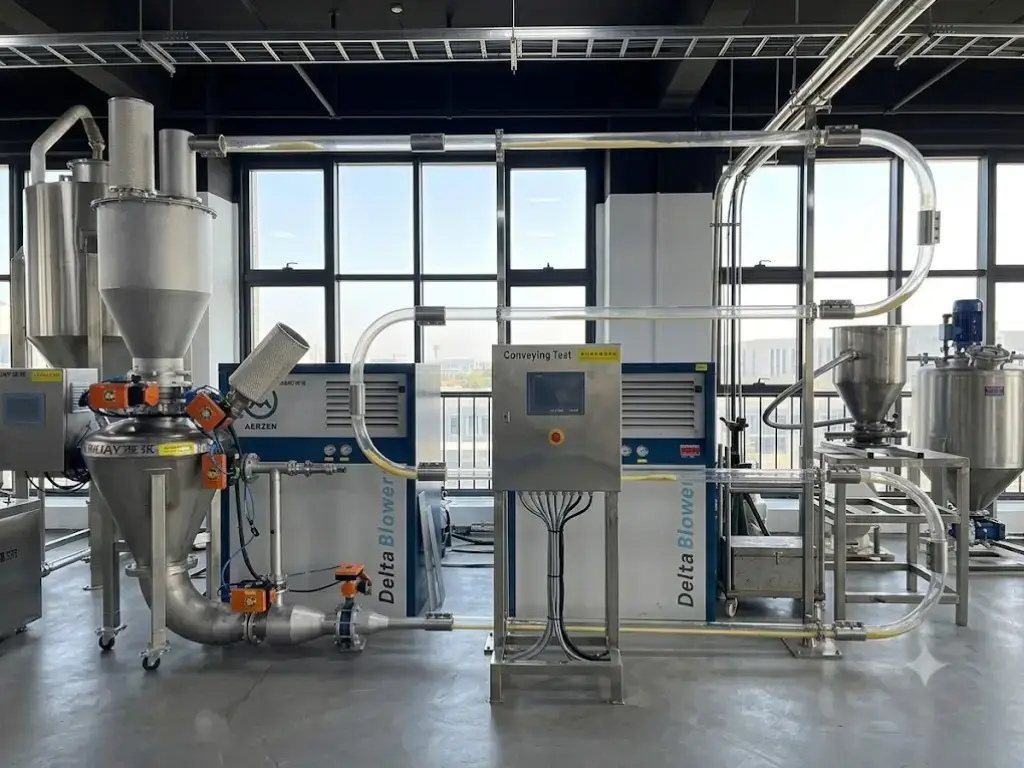
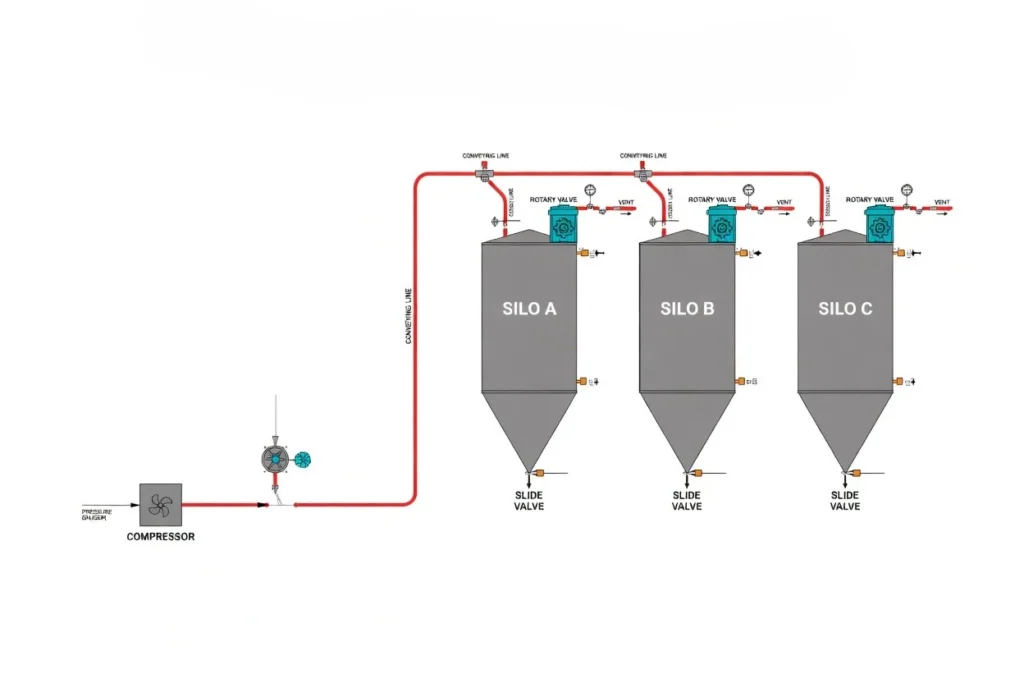
Dense phase conveying uses high pressure and low velocity. Material moves as a plug or dense slug. The air does not need to keep every particle suspended at high speed. For fragile materials, low velocity means fewer impacts. For abrasive materials, low velocity means less sliding and impact wear against the pipe wall. That is why dense phase is often the better starting point for both fragile and abrasive duties.
There is an important nuance: not all dense phase systems are equal. Conventional dense phase systems may empty the pipeline after each cycle. That empty-and-refill action creates acceleration zones and higher particle velocities, especially at the start and end of the cycle. A full-line dense phase concept takes a different approach. The pipeline starts and stops full of material. This reduces the repeated acceleration that damages fragile particles and wears abrasive ones.
Why Full-Line Dense Phase Works for Fragile Materials
Fragile materials such as pelletized carbon black, dry breakfast cereal, roasted peanuts, fertilizer pellets, and many polymer pellets need gentle handling. The goal is to avoid breakage, fines, dust, and product quality loss.
Full-line dense phase supports gentle handling in three ways:
- Low velocity. Particles move slowly as a coherent plug.
- Fewer acceleration events. Because the line does not empty after every cycle, the material is not repeatedly accelerated from zero.
- Controlled air injection. Air savers or boosters along the pipeline add air only where needed to keep the plug moving. This prevents pressure spikes and velocity surges.
Details matter. A poorly aligned pipe joint, a sharp elbow, or a valve with a leading edge can create a pinch point where pellets break. In one field case, a food processor was conveying roasted peanuts with a dilute phase system. Breakage and fines were high, and the customer was losing product value. After testing, the duty was moved to a full-line dense phase system with long-radius bends, smooth internal transitions, and carefully placed air boosters. The product arrived with visibly fewer fines, and the customer reduced rejection rates. The system was not magic. It was simply designed around the material instead of around the pipe.
Why Abrasive Materials Also Benefit from Low Velocity
Abrasive materials such as sand, glass batch, refractory batch, and mineral powders can destroy a pneumatic conveying system from the inside. In dilute phase, particles hit elbows at high speed. Wear is not linear with velocity; it is often described as proportional to velocity cubed. That means a small increase in velocity can create a large increase in wear. If you double velocity, wear potential can increase by roughly eight times. This is why “more air” is rarely the answer for abrasive materials.
Dense phase full-line conveying keeps velocity low and minimizes particle-to-pipe contact. It also changes the pipeline material conversation. With conventional high-velocity systems, plants often buy expensive wear-resistant pipe, ceramic-lined elbows, or special alloys. With a properly designed full-line dense phase system, standard schedule 40 mild steel pipe is often sufficient for many abrasive materials. For corrosive materials, standard schedule 10 stainless steel may be appropriate. The savings in pipeline cost and replacement labor can be substantial.
In one glass batch application, a plant was replacing a dilute phase elbow every few months. The material was abrasive, the velocity was high, and maintenance was disruptive. After reviewing the layout, rate, and particle size, the system was converted to full-line dense phase with a lower conveying velocity and fewer transitions. The wear problem dropped dramatically. The plant did not need a more exotic pipe. It needed a better conveying concept.
Choosing the Right System: A Comparison of Priorities
The right choice depends on the material, distance, capacity, layout, and operating profile. A simple comparison helps:
- Fragile material: prioritize low velocity, full-line dense phase, smooth transitions, and gentle start/stop.
- Abrasive material: prioritize low velocity, full-line dense phase, minimal elbows, and correct pipe material.
- Long distance or high rate: dense phase often provides a better balance of product care and reliability.
- Short distance, low rate, non-abrasive: dilute phase can be a practical and economical choice.
- Corrosive material: consider stainless steel or other suitable materials, but still control velocity.
- High moisture or sticky material: testing is essential; not every material behaves like dry sand or cereal.
The mistake is treating pneumatic conveying as a commodity. It is not. Two systems with the same pipe diameter can perform completely differently based on pressure, air injection, cycle logic, and layout. That is why material testing and application engineering matter more than a catalog selection.
What to Test Before You Buy
A reputable supplier should not guess. They should test. Useful tests include:
- Material bulk density, particle size, and shape.
- Degradation sensitivity for fragile products.
- Abrasion tendency for wear assessment.
- Minimum conveying velocity and pressure requirements.
- Start-up and shut-down behavior in full-line mode.
- Layout constraints, including vertical lifts, bends, and distance.
Testing does not need to be complicated, but it must be relevant. A test that uses the wrong velocity or the wrong cycle logic can give misleading results. The goal is to confirm that the system can move the material at the required rate without damaging the product or the pipeline.
Five FAQs About Dense Phase Pneumatic Conveying
1. Can one pneumatic conveying system handle both fragile and abrasive materials?
Yes, in many cases. The common factor is low velocity. A full-line dense phase system with proper air control can gently move fragile pellets and slowly move abrasive powders. However, material testing is needed because sticky, wet, or unusually shaped materials may require a different approach.
2. Is dense phase conveying slower than dilute phase?
The air velocity is lower, but the system can still achieve high throughput by using higher pressure and larger pipe sizes. “Slower air” does not automatically mean “lower production.” It often means less breakage and less wear.
3. Do I need expensive wear-resistant pipe for abrasive materials?
Not always. Full-line dense phase systems often use standard schedule 40 mild steel pipe for abrasive materials and schedule 10 stainless steel for corrosive materials. The key is keeping velocity low and minimizing impact points.
4. What is the full-line concept?
In a full-line dense phase system, the conveying pipeline starts and stops full of material. The pipe is not emptied after each cycle. This reduces acceleration and deceleration of particles, which lowers degradation and wear.
5. How do I choose between dense phase and dilute phase?
Start with the material and the application. If the product is fragile, abrasive, or the distance/rate is demanding, dense phase is usually the better starting point. If the material is robust, non-abrasive, and the duty is short and light, dilute phase may be sufficient. The final decision should be based on testing and engineering analysis.
Conclusion: Design Around the Material, Not the Pipe
Pneumatic conveying can handle both fragile and abrasive materials, but only when the system is designed around the material’s behavior. The contrast is clear: dilute phase uses speed; dense phase uses control. Dilute phase may be simple; full-line dense phase is often smarter for difficult duties. Fragile products need low-impact handling. Abrasive products need low-velocity handling. Both benefit from a system that does not empty the line after every cycle.
If you are evaluating custom dense phase pneumatic conveying systems for fragile and abrasive materials, the best next step is a practical engineering review. Wijay Systems works with processors to review material data, test conveying behavior, and configure a system that fits the real operating conditions. You do not need to overbuy exotic pipe or accept product breakage as normal. A better conveying concept can often solve both problems at once. When you are ready to discuss your application, our engineers are available to help.